TECHNICAL 05 · COATING
Pre-galvanised coil or hot-dip after fabrication: the choice that decides where rust starts.
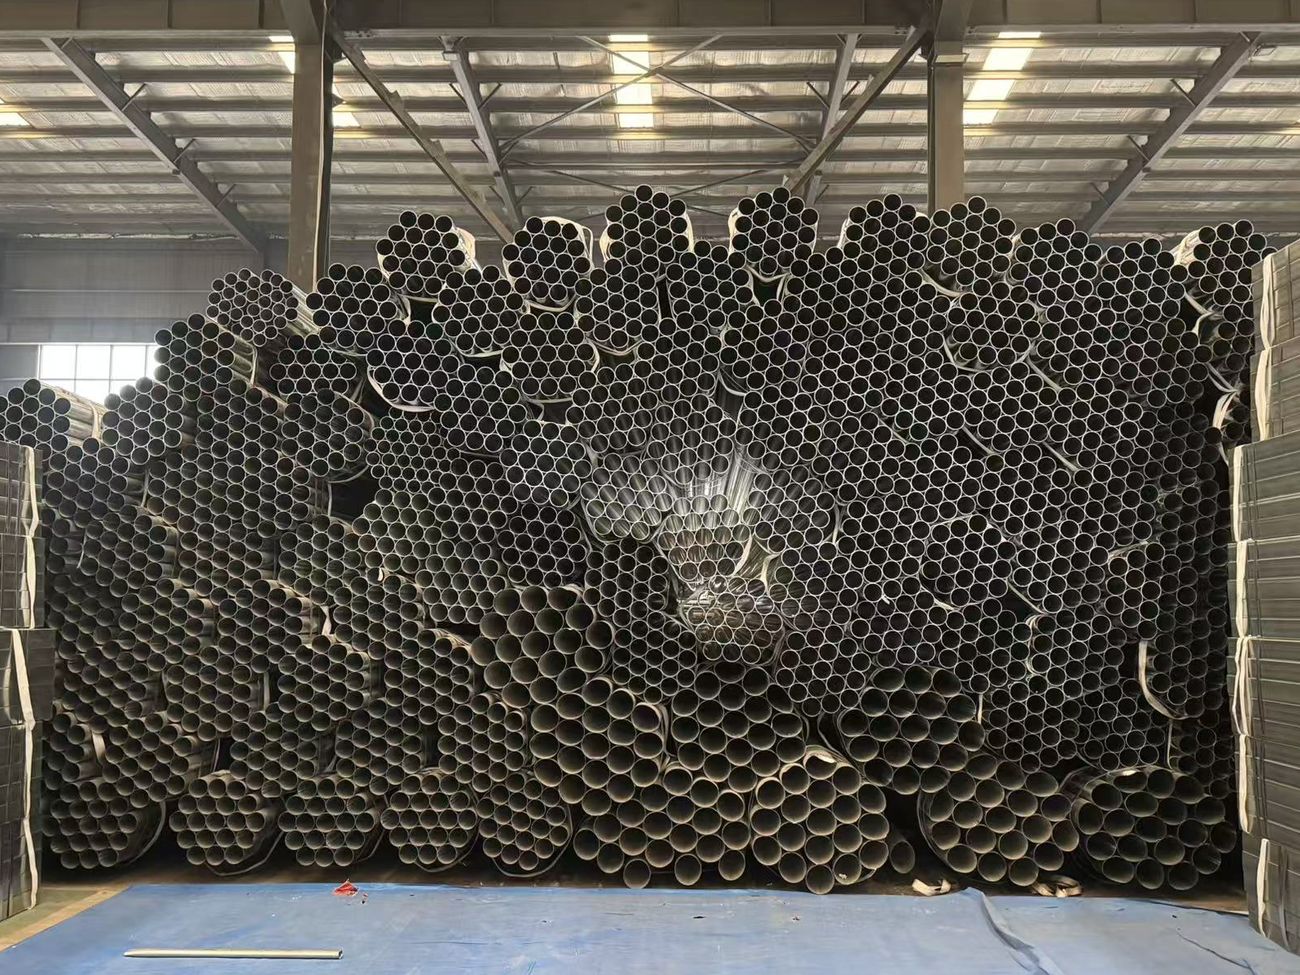
Two methods, two different protection patterns. Pre-galvanised protects the surface it was rolled with and leaves every cut end bare. Hot-dip coats the finished part, inside and out, including welds and cut ends.
| Pre-galvanised (Z275 coil) | Hot-dip (ISO 1461) | |
|---|---|---|
| When coating happens | At the steel mill, on coil | After fabrication, on the finished part |
| Cut ends | Bare steel | Coated |
| Welds | Bare, unless touched in | Coated |
| Coating thickness | ≈ 20 μm per side (275 g/m² total) | Typically 45–85 μm, class-dependent |
| Inside of tube | Coated as rolled | Coated if vented for dipping |
| Surface | Smooth, uniform | Slightly rougher, drain marks possible |
| Typical use | Roll-formed purlins, gutters, arches from coil | Welded frames, columns, humid sites |
| Cost | Lower | Higher, plus handling |
Z275 means 275 g/m² total zinc across both surfaces; that is about 137.5 g/m² per side, roughly 19–20 μm.
Where pre-galvanised fails first
- A cut end: no zinc at all, and the wall is exposed.
- A punched hole: the punch drags coating away at the edge.
- A weld: the heat destroys the coating for a zone around it.
- A rub point in a bundle: coating worn off in transit.
All four are fixable — touch-in with a zinc-rich coating, edge protection in packing, and a written requirement that field cuts be touched in. What is not fixable is a buyer discovering it two years later.
Where hot-dip is the right answer
Humid climates, coastal sites, livestock buildings with ammonia, glasshouses where the frame must last decades, and any project where the inspector will check coating thickness at a weld. In those cases the extra cost is a fraction of the frame and it removes an argument.
One limitation of hot-dip
Long tube must be vented so the zinc can flow and the air can escape; sealed hollow sections cannot be dipped properly. If a design needs sealed sections, say so early — the detail changes before fabrication, not after.
A specification sentence that works
“All steel to be hot-dip galvanised to ISO 1461 after fabrication, minimum coating 55 μm, with venting and draining holes as required; cut ends and field cuts to be touched in with zinc-rich coating supplied with the order.” That is a sentence an inspector can test.
Read next
Pages that answer the question this page raises.
- 08.06Zinc coating standardsZinc coating standards for greenhouse steel: Z275 mass coating, ISO 1461, ASTM A123 and GB→
- 04.01Round steel tubeRound galvanised steel tube for greenhouses: 1/2″ to 4″ outside diameter, wall 1.0–4.0 mm,→
- 07.04NigeriaGreenhouse frames for Nigeria: Lagos and Port Harcourt, tropical humidity, corrosion, coat→
- 08.C2Welded vs clampedWelded versus bolted/clamped greenhouse frames: stiffness, coating, shipping, erection and→
NEXT STEP
Turn this into a quoted frame list
If this page answered the technical question, the next step is a number. Send the parameters and we will price the tube, profiles, gutters and fittings as one package.